Bakerwall is a professional manufacturer of movable partition walls and vertical folding retractable wall systems. With over 15 years of engineering experience, we develop custom operable wall solutions for hotels, banquet halls, office buildings, conference centres and multi-purpose commercial spaces across more than 30 countries. Our core focus is delivering reliable space-dividing products with certified acoustic and fire performance, tailored to each project’s architectural requirements.
Our engineering team has completed hundreds of commercial partition projects worldwide. We have accumulated hands-on experience solving real challenges such as noise isolation, space flexibility, building code compliance and seamless installation. Our movable partition systems are laboratory-tested to achieve acoustic ratings up to RW62, allowing large venues to be split into independent functional rooms without permanent structural renovations.
We own our production facility and in-house technical lab, covering product R&D, prototype testing, precision manufacturing and technical drawing support. Our product range includes manual operable walls, semi-automatic movable partitions and fire-rated partition panels with HPL and HDF surface options.
We support both standard production and custom OEM & ODM orders, adapting dimensions, finishes and hardware to match project designs. Every batch undergoes strict quality inspection before shipment to guarantee long-term stability.
Product safety and performance are our top priorities. Our fire-rated and acoustic movable partitions have passed third-party testing and obtained relevant building material certifications. All technical parameters stated on our product pages are based on official test reports.
We maintain a full quality control workflow from raw material incoming inspection, panel fabrication to finished product testing, to reduce on-site project risks. You can view our [certification documents] for reference when evaluating partition solutions.
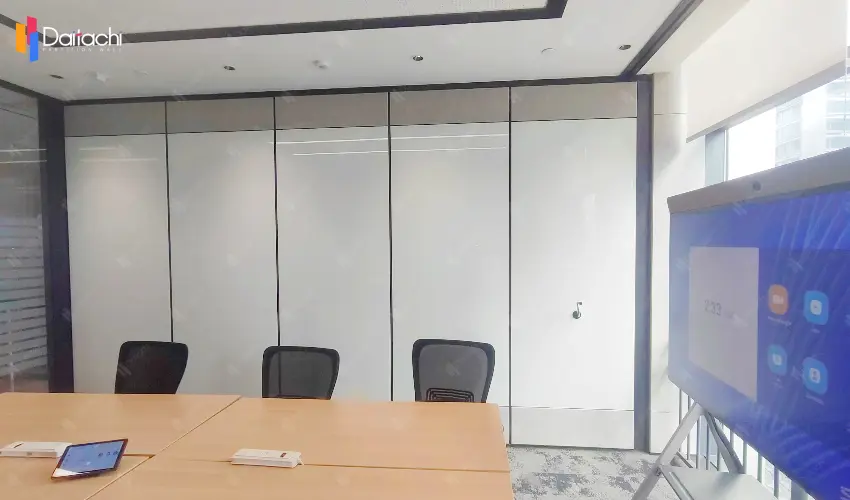
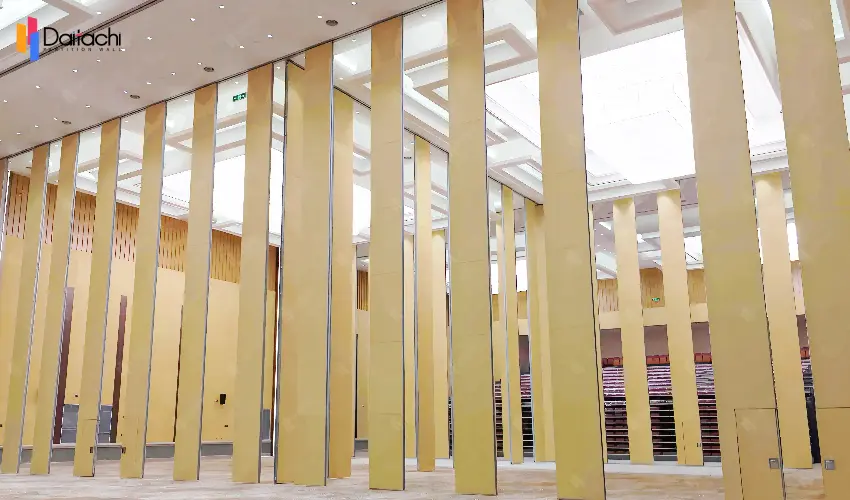
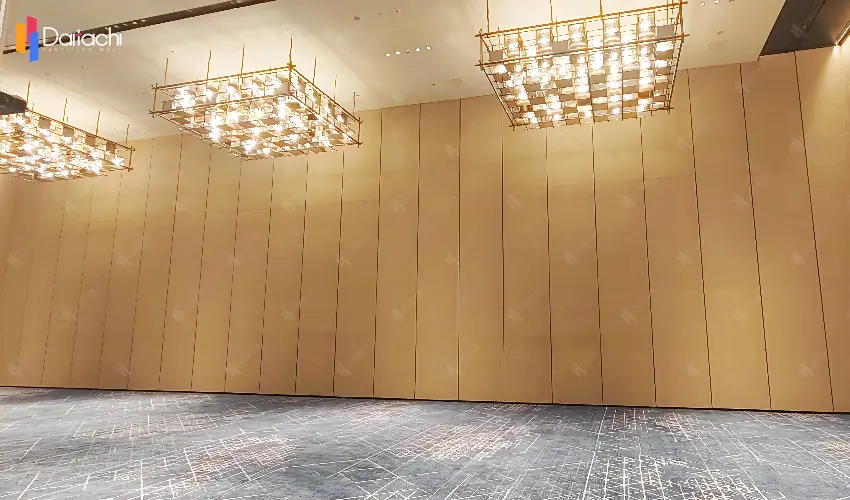
We have supplied partition walls for hospitality, corporate and public commercial projects. Our completed project portfolio covers ballrooms, meeting rooms, exhibition halls and restaurant flexible spaces. You can browse our real site photos and project details on our [project cases page] to see how our movable partitions work in real commercial environments.
Our technical team consists of partition design engineers and acoustic specialists who focus on movable wall system development, performance testing and project technical support. This team creates our technical guides and product documentation, including the articles published on our [news]. They provide professional suggestions for space layout, sound insulation and fire safety requirements for global clients.
1. Client inquiry and requirement confirmation
2. Custom layout drawing and technical proposal
3. Quotation and contract confirmation
4. Production, inspection and packaging
5. Shipment and installation guidance
Additional frequently asked questions are documented in the [FAQ] section. We provide remote technical guidance for all movable partition projects, covering both installation and after-sales support.
We aim to provide practical, durable and code-compliant movable partition systems to help building owners maximise space utilisation. We focus on transparent communication, accurate technical data and reliable product quality instead of exaggerated marketing claims.
Need custom movable partition solutions for your project?
Contact our engineering team for detailed technical drawings and quotation.
[Button: Get A Quote]